Solder bars for wave soldering and THT/PTH assembly
Lead-free and tin-lead bars for wave and selective solder pots, in 25 kg boxes
Dixtra Electronic bars are used to fill and top up the solder pots of wave soldering machines, where the through-hole (THT) components of printed circuit boards are soldered. Dickmann manufactures them to EN ISO 9453:2020 in the lead-free alloys most widely used in wave soldering and, for applications where lead is permitted, in traditional tin-lead alloys. To choose the alloy, see also the lead-free alloys.
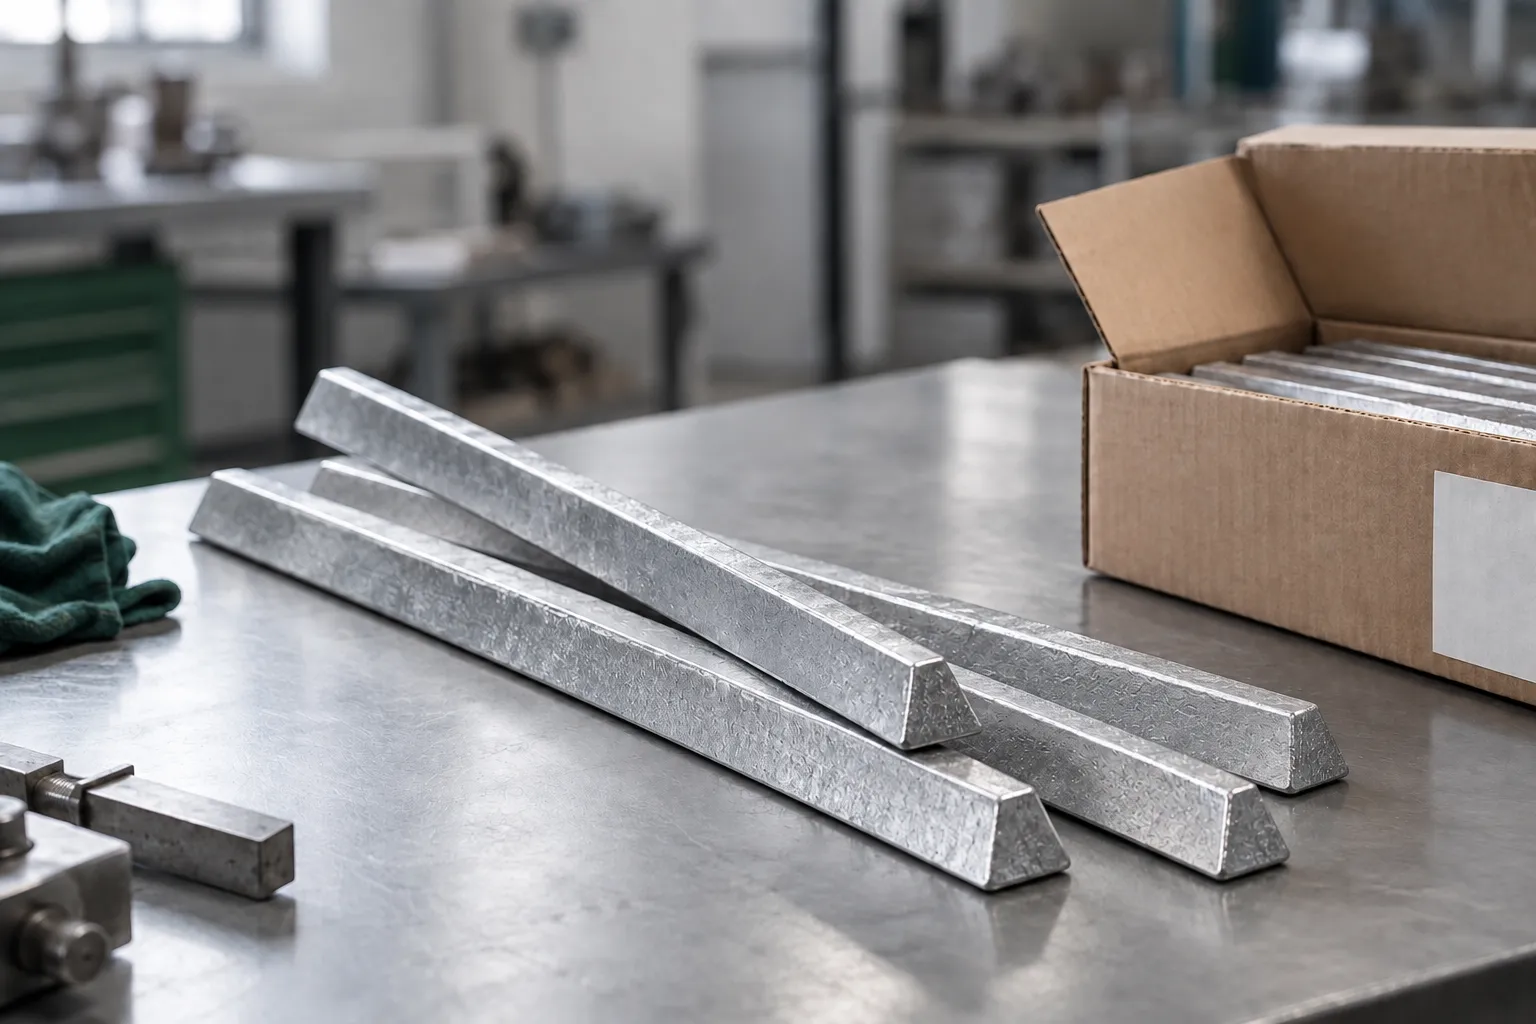
The Dixtra Electronic bar
- Cross-section
- Trapezoidal, 25 mm at the base and 8 mm at the top, 25 mm high
- Length
- 330 mm at the base, 315 mm at the top
- Weight
- Approx. 1 kg per bar, depending on the alloy
- Marking
- DIXTRA ELECTRONIC embossed
- Packaging
- 25 kg boxes
- Minimum order
- One 25 kg box
- Standard
- EN ISO 9453:2020 (except 63Sn35Pb2Ag), metals with purity above 99.9 %
Each lot is supplied with a certificate of analysis. Codes and alloys are also in the solder bar catalogue.
Alloys available as bars
Melting temperatures: typical values (solidus–liquidus).
| Alloy | Composition | Melting | When to choose it |
|---|---|---|---|
| 99SnCuNiGe (SN100C equivalent) | Sn/Cu0.7/Ni0.05/Ge | 227 °C | Silver-free, less dross and copper erosion |
| SAC0307 | Sn99/Ag0.3/Cu0.7 | 217–227 °C | Low silver, lower cost in solder baths |
| SAC305 | Sn96.5/Ag3/Cu0.5 | 217–220 °C | When the specification calls for SAC305 |
| Sn99.3Cu0.7 | Sn99.3/Cu0.7 | 227 °C | Silver-free, the most economical |
| Sn96.5Ag3.5 | Sn96.5/Ag3.5 | 221 °C | Eutectic, bright joints |
| 63Sn37Pb | Sn63/Pb37 | 183 °C | Eutectic tin-lead, where permitted |
| 60Sn40Pb | Sn60/Pb40 | 183–190 °C | Traditional tin-lead, where permitted |
| 63Sn35Pb2Ag | Sn63/Pb35/Ag2 | See technical sheet | Tin-lead with silver, where permitted |
Tin-lead alloys are for uses where lead is permitted: products outside the scope of the RoHS Directive, applications covered by exemptions in force, or destined for non-EU markets. 63Sn35Pb2Ag is a Dickmann alloy not covered by the EN ISO 9453 standard.
Managing the wave solder bath
With lead-free alloys the wave solder bath typically runs between 255 and 265 °C with SAC305 and SAC0307, and between 260 and 270 °C with Sn99.3Cu0.7 and 99SnCuNiGe, which melt at 227 °C. The right setting depends on the board, the contact time and the machine manufacturer's recommendations.
During production the bath dissolves copper from pads and component leads and picks up iron from the machine parts. When copper and iron exceed certain levels, the alloy becomes less fluid and bridging and icicles increase: this is why the bath must be analysed periodically and, if necessary, diluted or replaced.
- Top up with bars from the same alloy family as the bath: small, frequent additions keep level and temperature stable. When the analysis shows high copper, use the copper-free version (Sn99.7Ag0.3 for SAC0307, 99SnNiGe for 99SnCuNiGe).
- Remove dross from the surface of the solder pot regularly; a nitrogen atmosphere reduces its formation.
- Do not mix different alloys: between compatible lead-free alloys you can change over by gradual dilution, verified by analysis; from tin-lead to lead-free the solder pot must be completely emptied, cleaned, flushed with pure tin and the bath analysed for lead and iron.
- Have the bath analysed at regular intervals, depending on the volumes and boards produced.
For board fluxing see the alcohol-based and VOC-free no-clean fluxes; in selective soldering the bars fill the solder pot and solid wire tops it up automatically.
Bath analysis and dross recovery
Dickmann analyses customers' solder baths: just send a sample of at least 250 grams of alloy and you receive an impurity report with recommendations for correcting them. Dross and other process residues can be returned for recovery. Full details on the analysis and recovery services page.
THT or PTH?
THT (Through-Hole Technology) is the assembly technology for through-hole components; PTH (Plated Through Hole) is the plated hole in the circuit board into which the component lead is inserted. In Italy many EMS providers call THT assembly “PTH assembly”. Wave soldering solders all the THT components of a board in a single pass; for mixed-technology boards with few THT components, selective soldering is often used. See the guide to selective soldering and to consumables for electronics soldering.
Frequently asked questions about wave soldering bars
Request a quote for solder bars
Tell us the alloy, the number of 25 kg boxes and your annual consumption