Solder for sheet-metal work: 33 %, 40 %, 50 % or 60 %, differences and use on zinc and sheet metal
For sheet-metal solder sticks, the number indicates the percentage of tin: a 50/50 contains 50 % tin and 50 % lead, a 60/40 contains 60 % tin. Changing the tin content changes the melting range, how easily the bead can be shaped and the cost. This guide explains how to choose the tin content for gutters, flashings, titanium zinc and galvanised sheet.
Dickmann Srl · updated
Tin contents compared
All the alloys in this table begin to melt at 183 °C. What changes is the liquidus: the more lead the alloy contains, the higher the temperature at which it becomes completely liquid and the wider the pasty range in which the bead can be worked.
| Alloy | Solidus / liquidus | Typical use | Dickmann availability |
|---|---|---|---|
| Sn 33 / Pb 67 | 183 / about 250 °C | Heavy work where appearance does not matter | On request |
| Sn 35 / Pb 65 | 183 / 245 °C | Economical sheet-metal work, rough joints | On request |
| Sn 40 / Pb 60 | 183 / 238 °C | Sheet-metal work and titanium zinc | On request |
| Sn 50 / Pb 50 | 183 / 215 °C | Zinc, sheet-metal work and coffin liners | Immediately available from stock |
| Sn 60 / Pb 40 | 183 / 190 °C | Fine soldering, stained glass, build-up | Immediately available from stock |
Temperatures according to EN ISO 9453; for 33/67, which is not standardised, the value is indicative. Standard Dickmann solder sticks have a 10 × 6 mm half-moon cross-section, are 41 cm long and are packed in 25 kg boxes.
Why 50/50 is used
50/50 combines a wide pasty range, about 32 °C, with enough tin for good wettability on zinc. The sheet-metal worker can spread and shape the bead while the alloy solidifies, producing watertight joints on gutters, downpipes and flashings. For the same reason it is the alloy used for sealing zinc coffin liners. For titanium zinc, manufacturers specify 40/60 or 50/50 alloys with low antimony (Sb < 0.5 %): antimony makes the joint on zinc brittle.
Lower and higher tin contents
Lower tin contents, 33, 35 or 40 %, cost less because they contain less tin and have an even wider pasty range. They are suitable for heavy work where appearance matters little, but need higher temperatures to become liquid.
60/40 is near-eutectic: it melts between 183 and 190 °C, flows well and gives bright joints, but stays pasty only briefly. It is suitable for fine soldering, art stained glass and build-up, less so for long beads on zinc.
How to solder zinc and galvanised sheet
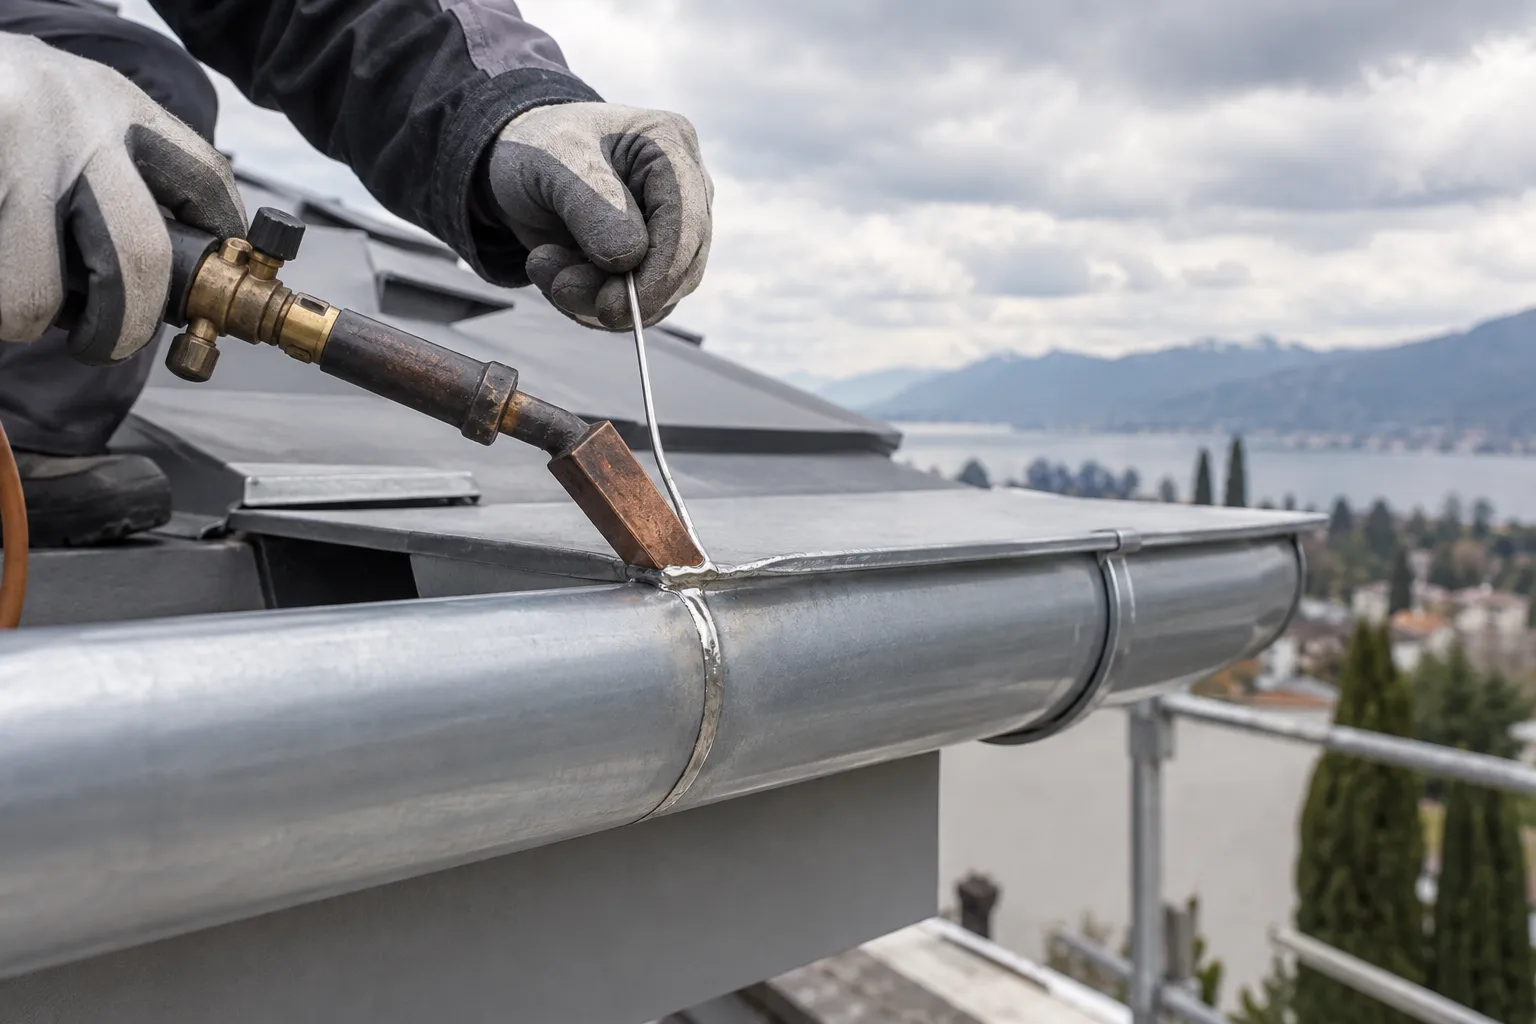
50/50 melts between 183 and 215 °C, well below the melting point of zinc (419 °C): even so, avoid overheating the sheet, which can burn through.
- Clean the surface of grease, oxides and dirt.
- Apply a flux specific for zinc and titanium zinc, based on zinc and ammonium chlorides, preferably the one specified by the sheet manufacturer. Titanium zinc producers advise against neat muriatic acid, which is harmful to the operator, the tools and the sheet.
- Heat with a gas or electric soldering iron of adequate power: about 250 °C is needed in the joint area, above the liquidus of the alloy.
- Spread the alloy and shape the bead during the pasty phase.
- Let it cool without moving the joint and immediately remove the flux residues with a damp cloth: they are corrosive.
Lead and regulations
Gutters, flashings and coffin liners are not electrical and electronic equipment: the RoHS Directive does not apply and tin-lead alloys remain the traditional choice. Other applicable regulations and the safety data sheet instructions on handling lead must nevertheless be complied with. See the guide to RoHS exemptions for lead.